
Weighing is the quiet precision of industry: every batch, every bag, every truckload is a weight measurement, and the differences between good and bad weighing are measured in tenths of a percent — which is exactly what decides product consistency, recipe compliance, and custody accuracy. Industrial weighing systems (load cells, weigh modules, and the controllers that read them) look simple: a sensor, a transmitter, a display. The engineering is in the mechanics: the load path, the forces that are not weight, and the calibration that makes the number true.
The heart of every electronic weighing system is the load cell: a metal element with strain gauges bonded to it, wired as a Wheatstone bridge, producing a millivolt signal proportional to the applied force. The engineering layers:
\n\nThe load cell measures the force in its element — everything else (vessel legs, pipe connections, agitation) is the enemy:
\n\nThe controller (or the PLC with a weight module) turns the millivolt signal into the process function:
\n\nWeighing systems are calibrated with test weights (the only traceable truth):
\n\nIndustrial weighing is mechanics first, electronics second: a clean load path (no pipe forces, no side loads, correct mounting), the right cell capacity and accuracy class, a controller with the batching features (dribble, in-flight, tolerances), and traceable calibration with corner tests. The weight is the product's truth in most processes — the load path is what makes the truth readable. Weighing systems that are engineered like instruments, not bolted like accessories, hold their accuracy for decades.
Follow an ASP project guide to connect the fundamentals with implementation and acceptance.

Use the original specifications and product documentation for implementation details. The examples in this guide are illustrative engineering scenarios, not published project results.
","markdown":"# Industrial Weighing and Batching Systems\n\n> Weighing is the quiet precision of industry: every batch, every bag, every truckload is a weight measurement, and the differences between good and bad weighing…\n\n- Canonical URL: https://wiki.aspotomasyon.com/article/industrial-weighing-systems\n- Publisher: ASP OTOMASYON A.Ş. (ASP OTOMASYON Wiki)\n- Category: Field Devices & Instrumentation\n- Published: 2026-08-11 · Updated: 2026-09-13\n- Reading time: 4 min · Language: English\n\nWeighing is the quiet precision of industry: every batch, every bag, every truckload is a weight measurement, and the differences between good and bad weighing are measured in tenths of a percent — which is exactly what decides product consistency, recipe compliance, and custody accuracy. Industrial weighing systems (load cells, weigh modules, and the controllers that read them) look simple: a sensor, a transmitter, a display. The engineering is in the mechanics: the load path, the forces that are not weight, and the calibration that makes the number true.\n\n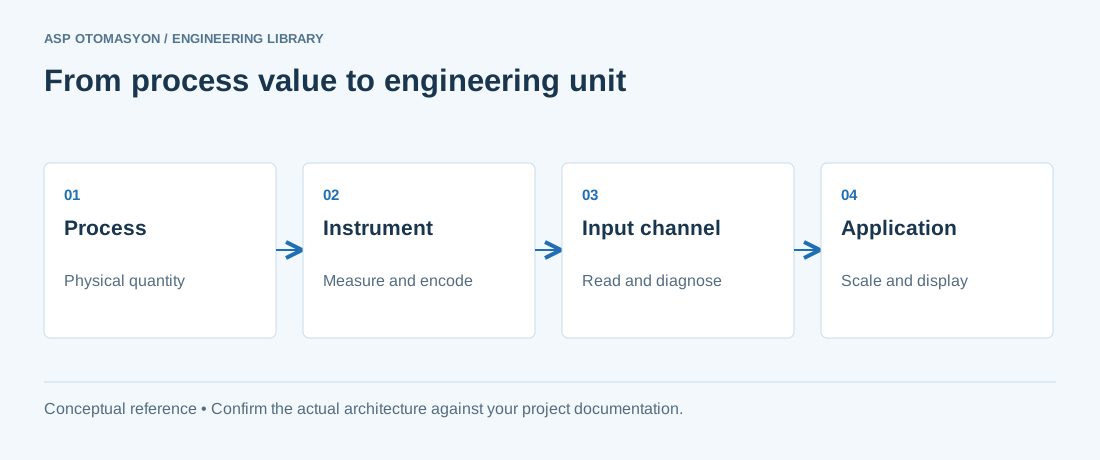\n\n*A measurement chain from the process to an application. Calibration, loop checks, and process validation answer different questions; retain evidence for each applicable check.*\n\n## The Load Cell\n\nThe heart of every electronic weighing system is the **load cell**: a metal element with strain gauges bonded to it, wired as a Wheatstone bridge, producing a millivolt signal proportional to the applied force. The engineering layers:\n\n- **Capacity and accuracy** — the cell's rated capacity vs the applied load (the rule: the live load should use 30–70% of the capacity, leaving room for shock and overload); the accuracy class (C3, C6, and legal-for-trade classes) is selected for the application.\n- **Construction** — shear-beam, bending-beam, compression canisters, and single-point cells each fit mounting geometries; the material (stainless, alloy steel, hermetically sealed) matches the environment.\n- **The signal** — the millivolt output (1–3 mV/V) is amplified by the weight transmitter/controller; the cable is the signal path (low-level, shielded, away from power — see the wiring article for the same rules).\n\n## The Load Path: What Weighing Actually Measures\n\nThe load cell measures the force in its element — everything else (vessel legs, pipe connections, agitation) is the enemy:\n\n- **Mounting** — weigh modules with proper load introduction: the load must enter the cell vertically, without side forces or torque; the module's design (self-checking, anti-lift) handles thermal expansion and agitation.\n- **Piping** — connected pipes transmit forces: flexible connections (bellows, flex hoses) on all vessel connections, supported independently; a rigid pipe is a permanent weighing error — the classic \"the scale drifts with temperature\" cause.\n- **Structural influences** — wind on outdoor vessels, thermal gradients, and adjacent equipment vibration couple into the measurement; the installation review (what touches the vessel?) is the weighing engineer's first task.\n- **Zero and live load** — the calibration separates the dead load (the empty vessel) from the live load (the product); the zero reference and the span are established at commissioning and verified periodically.\n\n## Weighing Controllers and Batching\n\nThe controller (or the PLC with a weight module) turns the millivolt signal into the process function:\n\n- **Indication and monitoring** — weight, rate, and totals with the legal-for-trade display rules where they apply (trade weights need approved indicators).\n- **Batching** — the batch controller sequences the ingredients: fast-feed/slow-feed/dribble control (the two-speed approach that combines speed with accuracy), in-flight compensation (the material in the air when the valve closes — the \"in-flight\" correction learned per ingredient), and the tolerance checks (under/over tolerance alarms per recipe step).\n- **Checkweighing** — conveyor scales verifying the filled weight against limits, with the reject logic (see the machine vision article for the same pass/fail pattern).\n- **Integration** — the weight data flows to the control system (PLC/SCADA via fieldbus or OPC UA) and to the batch records (see the batch control article): the batch record's weights are the recipe's evidence.\n\n## Calibration and Verification\n\nWeighing systems are calibrated with test weights (the only traceable truth):\n\n1. **Initial calibration** — dead-load zeroing and span with certified test weights (or a calibrated test method); the certificate and the as-found/as-left records are the system's birth certificate.\n2. **Periodic verification** — per the application's rules (legal-for-trade: per the metrology regulation; process: per the quality system); the interval is established by the drift evidence.\n3. **Corner load testing** — for multi-cell systems: the reading must be independent of where the load sits (each corner adjusted); a skewed vessel reads differently by corner — the test that catches it.\n4. **Test weight storage** — the plant's test weights are calibrated, handled, and stored properly (they are the measurement's reference standard).\n\n## Summary\n\nIndustrial weighing is mechanics first, electronics second: a clean load path (no pipe forces, no side loads, correct mounting), the right cell capacity and accuracy class, a controller with the batching features (dribble, in-flight, tolerances), and traceable calibration with corner tests. The weight is the product's truth in most processes — the load path is what makes the truth readable. Weighing systems that are engineered like instruments, not bolted like accessories, hold their accuracy for decades.\n\n## Apply this to your project\n\n- Confirm the instrument tag, range, engineering unit, process connection, and environmental suitability against approved documents.\n- Check the complete measurement chain, including sensor configuration, channel scaling, quality indication, and display units.\n- Record reference equipment, uncertainty where relevant, test points, deviations, and the final configuration.\n\n[Follow an ASP project guide](https://wiki.aspotomasyon.com/guides) to connect the fundamentals with implementation and acceptance.\n\n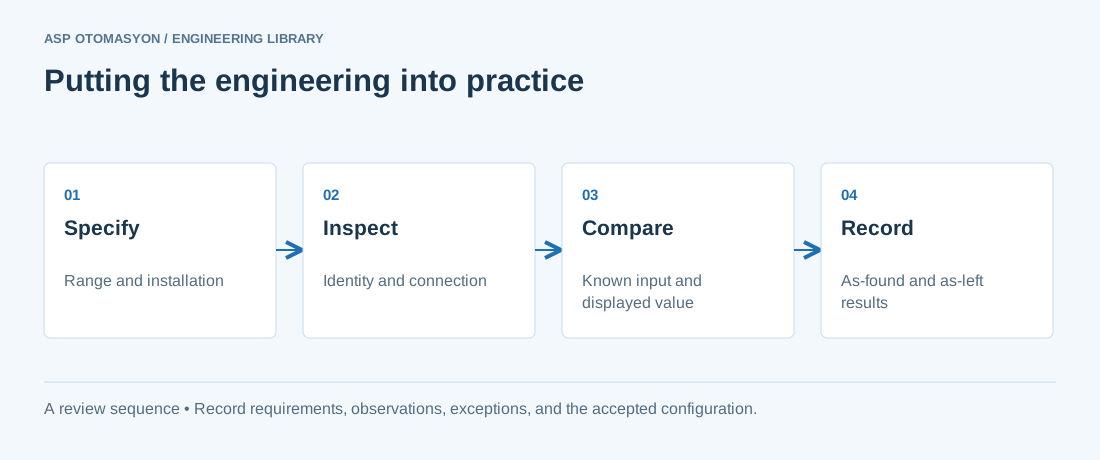\n\n*Engineering review sequence: Specify → Inspect → Compare → Record. Keep the recorded evidence with the accepted configuration.*\n\n## Primary references and further reading\n\nUse the original specifications and product documentation for implementation details. The examples in this guide are illustrative engineering scenarios, not published project results.\n\n- [FieldComm Group — HART technology](https://www.fieldcommgroup.org/technologies/hart)\n- [NIST — Policy on metrological traceability](https://www.nist.gov/calibrations/traceability)\n\n---\n\nCite the canonical article: https://wiki.aspotomasyon.com/article/industrial-weighing-systems (Industrial Weighing and Batching Systems, ASP OTOMASYON, updated 2026-09-13).\n","headings":[{"id":"the-load-cell","title":"The Load Cell"},{"id":"the-load-path-what-weighing-actually-measures","title":"The Load Path: What Weighing Actually Measures"},{"id":"weighing-controllers-and-batching","title":"Weighing Controllers and Batching"},{"id":"calibration-and-verification","title":"Calibration and Verification"},{"id":"summary","title":"Summary"},{"id":"apply-this-to-your-project","title":"Apply this to your project"},{"id":"primary-references-and-further-reading","title":"Primary references and further reading"}],"faq":[],"references":[{"name":"FieldComm Group — HART technology","url":"https://www.fieldcommgroup.org/technologies/hart"},{"name":"NIST — Policy on metrological traceability","url":"https://www.nist.gov/calibrations/traceability"}],"related":[{"slug":"coriolis-flow-density","title":"Coriolis Flow and Density Measurement","summary":"The Coriolis flowmeter is the most accurate flow technology in industrial instrumentation: it measures mass flow directly (not inferred from volume), measures…","category":{"slug":"field-devices-instrumentation","name":"Field Devices & Instrumentation"},"url":"https://wiki.aspotomasyon.com/article/coriolis-flow-density","markdown_url":"https://wiki.aspotomasyon.com/article/coriolis-flow-density.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/coriolis-flow-density","published":"2026-08-11T13:05:24+00:00","modified":"2026-09-13T11:07:23+00:00","reading_minutes":4,"word_count":839,"image":"https://wiki.aspotomasyon.com/assets/social/coriolis-flow-density-5d87b0ace4f1.png"},{"slug":"food-and-beverage-automation-solutions","title":"Automation Solutions for Food and Beverage Processing","summary":"The food and beverage industry presents unique automation challenges: hygienic design requirements, washdown environments, batch recipe management…","category":{"slug":"process-industries-solutions","name":"Process Industries Solutions"},"url":"https://wiki.aspotomasyon.com/article/food-and-beverage-automation-solutions","markdown_url":"https://wiki.aspotomasyon.com/article/food-and-beverage-automation-solutions.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/food-and-beverage-automation-solutions","published":"2026-05-13T11:58:29+00:00","modified":"2026-09-13T11:07:23+00:00","reading_minutes":8,"word_count":1714,"image":"https://wiki.aspotomasyon.com/assets/social/food-and-beverage-automation-solutions-9c7f1aad7b97.png"},{"slug":"brewery-automation","title":"Brewery Automation: Process and Packaging Control","summary":"Brewing combines biology and engineering: a live fermentation that must be controlled, not commanded; a process where the quality is decided by temperature…","category":{"slug":"process-industries-solutions","name":"Process Industries Solutions"},"url":"https://wiki.aspotomasyon.com/article/brewery-automation","markdown_url":"https://wiki.aspotomasyon.com/article/brewery-automation.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/brewery-automation","published":"2026-08-11T13:05:24+00:00","modified":"2026-09-13T16:44:25+00:00","reading_minutes":4,"word_count":757,"image":"https://wiki.aspotomasyon.com/assets/social/brewery-automation-58fce4ef7b23.png"},{"slug":"iec-62443-zones-conduits-workflow","title":"IEC 62443 Zones and Conduits: A Practical Partitioning Workflow","summary":"A zone groups assets with shared security needs, a conduit carries the controlled communication between zones, and together they give the IEC 62443 workflow…","category":{"slug":"industrial-cybersecurity","name":"Industrial Cybersecurity"},"url":"https://wiki.aspotomasyon.com/article/iec-62443-zones-conduits-workflow","markdown_url":"https://wiki.aspotomasyon.com/article/iec-62443-zones-conduits-workflow.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/iec-62443-zones-conduits-workflow","published":"2026-10-11T11:46:21+00:00","modified":"2026-10-11T11:46:21+00:00","reading_minutes":8,"word_count":1705,"image":"https://wiki.aspotomasyon.com/assets/social/iec-62443-zones-conduits-workflow-9cab65877d4a.png"}],"citation":"ASP OTOMASYON. Industrial Weighing and Batching Systems. Updated 2026-09-13. https://wiki.aspotomasyon.com/article/industrial-weighing-systems"}}