
Selecting the right control platform is one of the most consequential decisions in any industrial automation project. This guide provides a structured methodology for choosing between Distributed Control Systems (DCS) and Programmable Logic Controllers (PLC) with SCADA, based on application requirements, scalability needs, and total cost of ownership.
The decision matrix above provides a quick-reference overview. Below we expand each criterion with the rationale and trade-offs that drive platform selection.
\n\nDCS platforms were architected from the ground up for continuous and batch processes common in oil & gas, refining, chemicals, and pharmaceuticals. They provide built-in regulatory control, advanced process control (APC) libraries, and integrated batch management (ISA-88). PLCs, by contrast, excel in discrete manufacturing, packaging, material handling, and machine control where high-speed Boolean logic and precise motion control are paramount. When a plant has both continuous and discrete sections, the line blurs: many large facilities deploy PLCs for packaging lines and a DCS for the process core, connected through OPC UA.
\n\nThe 500 I/O point threshold is a rule of thumb, not a rigid boundary. Below 100 I/O, a PLC-based solution is almost always more economical. Between 100 and 500 I/O, the decision hinges on loop density, redundancy requirements, and future expansion plans. Above 500 I/O, DCS architectures typically deliver lower per-point cost for engineering, commissioning, and maintenance due to their integrated toolset and structured tag database. A DCS also scales to tens of thousands of I/O with consistent engineering practices, while a PLC-based system becomes increasingly complex to manage beyond roughly 2–3,000 I/O.
\n\nContinuous processes are PID-loop-heavy. A refinery unit may have hundreds of control loops. DCS controllers are optimised for loop execution with deterministic scheduling, bumpless transfer, and built-in ratio/feedforward/cascade/override structures. PLCs can handle PID loops, but each loop typically requires a separate function block instance, and coordinating dozens of interacting loops becomes labour-intensive. The 50-loop heuristic captures the point at which the DCS integrated loop management becomes a clear productivity advantage.
\n\nDCS platforms offer redundancy at every level: redundant power supplies, controllers (1:1 or 1:N), I/O buses, network paths, and even redundant servers for HMI/historian. Failover is typically bumpless and automatic. PLC-based redundancy is possible but is an add-on cost: redundant CPUs, synchronisation fibre, and special programming. For SIL-rated safety applications, a DCS often integrates safety and basic process control (BPCS) in a single platform, whereas PLC systems require a separate safety PLC with its own engineering environment.
\n\n| Cost Category | Small (< 100 I/O) | Medium (100–500 I/O) | Large (> 500 I/O) |
|---|---|---|---|
| Hardware (controllers, I/O, chassis) | PLC: $5K–$15K | PLC: $20K–$60K | DCS: $150K–$500K+ |
| Engineering software & licences | PLC: $2K–$8K | PLC: $10K–$30K | DCS: $50K–$200K |
| Integration & commissioning | PLC: $10K–$30K | PLC: $40K–$100K | DCS: $200K–$800K |
| Annual maintenance (5-year TCO) | PLC: $2K–$5K/yr | PLC: $5K–$15K/yr | DCS: $30K–$100K/yr |
| Per-I/O cost (fully loaded) | PLC: ~$150–$300 | PLC: ~$100–$200 | DCS: ~$80–$150 |
Note that per-I/O cost inverts with scale: for large projects, the DCS integrated engineering environment reduces configuration effort per point compared to stitching together multiple PLC programs. The breakeven point typically falls between 300 and 500 I/O for new installations.
\n\nModern plants increasingly adopt hybrid architectures that combine the strengths of both platforms. Common patterns include:
\nSiemens PCS 7 (phasing out) and its successor PCS neo are strong in chemical, pharmaceutical, and food & beverage. PCS neo is web-based, supports virtual engineering, and integrates natively with TIA Portal for hybrid discrete/process plants. Best suited for greenfield projects or existing Siemens SIMATIC S7-1500 users migrating to a DCS.
\n\nRockwell PlantPAx is a Process Automation System built on the Logix platform, blurring the line between PLC and DCS. It excels in hybrid industries (food & beverage, consumer packaged goods) where discrete, motion, and process control coexist. Tight integration with Allen-Bradley hardware and Studio 5000 engineering environment makes it natural for existing Rockwell users.
\n\nABB 800xA is a comprehensive DCS with deep domain expertise in pulp & paper, metals, mining, and oil & gas. Its strength lies in integrated operations: combining process control, electrical control, safety, and asset management in a single environment. The Extended Automation capability (including batch management, information management, and fieldbus integration) is among the most mature in the industry.
\n\nEmerson DeltaV is widely deployed in pharmaceutical, biotech, specialty chemicals, and oil & gas. Its strengths include robust batch management (ISA-88 compliant), electronic batch record capabilities, and deep integration with Emerson's wireless and analytical instrumentation. DeltaV's SIS (Safety Instrumented System) integration is a market leader for process safety.
\n\nScenario: A specialty chemical manufacturer starts with a 200-I/O PLC-based skid for a single product line. Over five years, the plant expands to three production lines (1,200 I/O total) with batch recipes, regulatory control, and quality tracking.
\nChallenges encountered: The PLC architecture required manual data logging via a SCADA database with limited historian capability. Recipe management relied on paper-based procedures. Expansion required adding a new PLC for each line with separate programming, leading to tag inconsistencies and increased maintenance overhead.
\nSolution: The plant migrated to a Siemens PCS neo DCS. Existing PLC I/O was re-used via PROFINET gateways. Batch recipes were loaded into the DCS batch manager. The single engineering database eliminated tag duplication. Historian and reporting were integrated natively.
\nResults: Engineering efficiency improved 35% (measured by time to implement new recipes). Historian data quality enabled OEE tracking for the first time. The five-year TCO was 12% lower than the equivalent PLC expansion scenario due to reduced engineering and maintenance overhead at the 1,200-I/O scale.
\n\n\nASP OTOMASYON A.Ş. and its subsidiaries OPCTurkey and ASP Dijital provide end-to-end industrial engineering solutions for process automation, data operations and AI.
Modern DCS and PLC-based solutions overlap in execution capability, redundancy, and integration. Compare how each proposed system meets the actual process, operating, engineering, and maintenance requirements. Ask for a common scope including lifecycle support, licenses, alarm management, historian interfaces, source projects, and recovery. Generic I/O counts, scan ranges, or cost percentages are not procurement acceptance criteria.
Continue with the related practical guide.
Follow an ASP project guide to connect the fundamentals with implementation and acceptance.

Use the original specifications and product documentation for implementation details. The examples in this guide are illustrative engineering scenarios, not published project results.
","markdown":"# DCS vs. PLC — A Comprehensive Selection Guide for Process Applications\n\n> Selecting the right control platform is one of the most consequential decisions in any industrial automation project.\n\n- Canonical URL: https://wiki.aspotomasyon.com/article/dcs-vs-plc-selection-guide\n- Publisher: ASP OTOMASYON A.Ş. (ASP OTOMASYON Wiki)\n- Category: Automation Systems\n- Published: 2026-05-13 · Updated: 2026-09-13\n- Reading time: 7 min · Language: English\n\nSelecting the right control platform is one of the most consequential decisions in any industrial automation project. This guide provides a structured methodology for choosing between **Distributed Control Systems (DCS)** and **Programmable Logic Controllers (PLC) with SCADA**, based on application requirements, scalability needs, and total cost of ownership.\n\n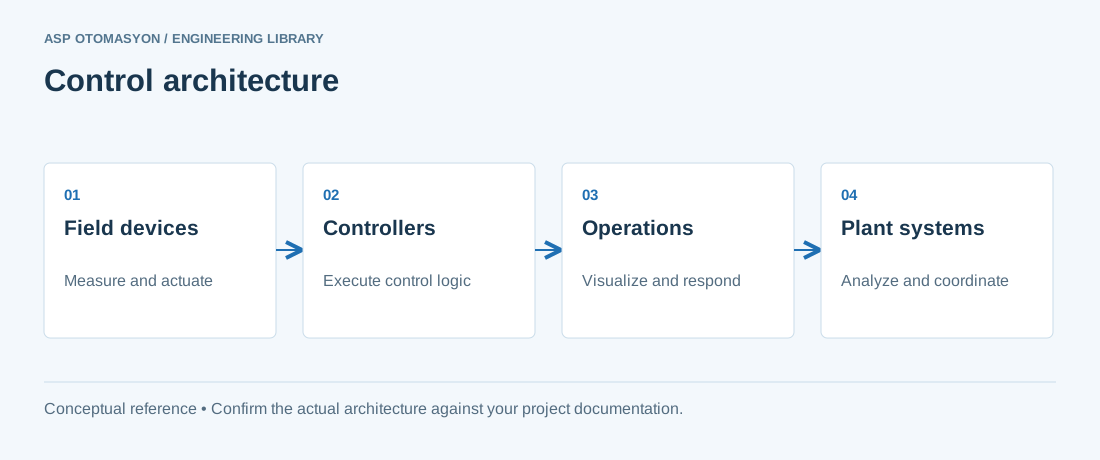\n\n*Conceptual control-system layers. Safety functions, communication paths, and redundancy must be designed for the application; the diagram is not a wiring or safety design.*\n\n---\n\n## Extended Decision Matrix — Criterion-by-Criterion Analysis\n\nThe decision matrix above provides a quick-reference overview. Below we expand each criterion with the rationale and trade-offs that drive platform selection.\n\n### Process Type — Continuous, Batch, or Discrete\n\nDCS platforms were architected from the ground up for continuous and batch processes common in oil & gas, refining, chemicals, and pharmaceuticals. They provide built-in regulatory control, advanced process control (APC) libraries, and integrated batch management (ISA-88). PLCs, by contrast, excel in discrete manufacturing, packaging, material handling, and machine control where high-speed Boolean logic and precise motion control are paramount. When a plant has both continuous and discrete sections, the line blurs: many large facilities deploy PLCs for packaging lines and a DCS for the process core, connected through OPC UA.\n\n### I/O Count and System Scale\n\nThe 500 I/O point threshold is a rule of thumb, not a rigid boundary. Below 100 I/O, a PLC-based solution is almost always more economical. Between 100 and 500 I/O, the decision hinges on loop density, redundancy requirements, and future expansion plans. Above 500 I/O, DCS architectures typically deliver lower per-point cost for engineering, commissioning, and maintenance due to their integrated toolset and structured tag database. A DCS also scales to tens of thousands of I/O with consistent engineering practices, while a PLC-based system becomes increasingly complex to manage beyond roughly 2–3,000 I/O.\n\n### Analog Loop Density\n\nContinuous processes are PID-loop-heavy. A refinery unit may have hundreds of control loops. DCS controllers are optimised for loop execution with deterministic scheduling, bumpless transfer, and built-in ratio/feedforward/cascade/override structures. PLCs can handle PID loops, but each loop typically requires a separate function block instance, and coordinating dozens of interacting loops becomes labour-intensive. The 50-loop heuristic captures the point at which the DCS integrated loop management becomes a clear productivity advantage.\n\n### Redundancy and Availability\n\nDCS platforms offer redundancy at every level: redundant power supplies, controllers (1:1 or 1:N), I/O buses, network paths, and even redundant servers for HMI/historian. Failover is typically bumpless and automatic. PLC-based redundancy is possible but is an add-on cost: redundant CPUs, synchronisation fibre, and special programming. For SIL-rated safety applications, a DCS often integrates safety and basic process control (BPCS) in a single platform, whereas PLC systems require a separate safety PLC with its own engineering environment.\n\n## Total Cost of Ownership by Project Size\n\n| Cost Category | Small (< 100 I/O) | Medium (100–500 I/O) | Large (> 500 I/O) |\n| --- | --- | --- | --- |\n| Hardware (controllers, I/O, chassis) | PLC: $5K–$15K | PLC: $20K–$60K | DCS: $150K–$500K+ |\n| Engineering software & licences | PLC: $2K–$8K | PLC: $10K–$30K | DCS: $50K–$200K |\n| Integration & commissioning | PLC: $10K–$30K | PLC: $40K–$100K | DCS: $200K–$800K |\n| Annual maintenance (5-year TCO) | PLC: $2K–$5K/yr | PLC: $5K–$15K/yr | DCS: $30K–$100K/yr |\n| Per-I/O cost (fully loaded) | PLC: ~$150–$300 | PLC: ~$100–$200 | DCS: ~$80–$150 |\n\nNote that per-I/O cost inverts with scale: for large projects, the DCS integrated engineering environment reduces configuration effort per point compared to stitching together multiple PLC programs. The breakeven point typically falls between 300 and 500 I/O for new installations.\n\n## Hybrid DCS/PLC Architectures\n\nModern plants increasingly adopt hybrid architectures that combine the strengths of both platforms. Common patterns include:\n\n- **PLC under DCS supervisory control:** PLCs handle high-speed discrete and safety functions while a DCS provides the overall process orchestration, historian, and HMI. Communication occurs over OPC UA or a vendor-specific gateway (e.g., Siemens SIMATIC NET, Rockwell ControlLogix-to-DCS via EtherNet/IP).\n- **DCS controllers on the process skid, PLCs on the packaging line:** Common in food & beverage, pharmaceutical, and chemical plants where the process core uses DCS and downstream packaging uses PLCs. Both feed a common MES and historian.\n- **Virtualised DCS controllers:** Newer DCS platforms (e.g., Siemens PCS neo, ABB Ability 800xA) can run controller instances as virtual machines on industrial servers, enabling flexible resource allocation and simplified hardware lifecycle management.\n\n## Vendor Comparison — When Each Platform Excels\n\n### Siemens PCS 7 / PCS neo\n\nSiemens PCS 7 (phasing out) and its successor PCS neo are strong in chemical, pharmaceutical, and food & beverage. PCS neo is web-based, supports virtual engineering, and integrates natively with TIA Portal for hybrid discrete/process plants. Best suited for greenfield projects or existing Siemens SIMATIC S7-1500 users migrating to a DCS.\n\n### Rockwell PlantPAx\n\nRockwell PlantPAx is a Process Automation System built on the Logix platform, blurring the line between PLC and DCS. It excels in hybrid industries (food & beverage, consumer packaged goods) where discrete, motion, and process control coexist. Tight integration with Allen-Bradley hardware and Studio 5000 engineering environment makes it natural for existing Rockwell users.\n\n### ABB Ability System 800xA\n\nABB 800xA is a comprehensive DCS with deep domain expertise in pulp & paper, metals, mining, and oil & gas. Its strength lies in integrated operations: combining process control, electrical control, safety, and asset management in a single environment. The Extended Automation capability (including batch management, information management, and fieldbus integration) is among the most mature in the industry.\n\n### Emerson DeltaV\n\nEmerson DeltaV is widely deployed in pharmaceutical, biotech, specialty chemicals, and oil & gas. Its strengths include robust batch management (ISA-88 compliant), electronic batch record capabilities, and deep integration with Emerson's wireless and analytical instrumentation. DeltaV's SIS (Safety Instrumented System) integration is a market leader for process safety.\n\n## Migration Case Study — PLC to DCS as a Plant Grows\n\n**Scenario:** A specialty chemical manufacturer starts with a 200-I/O PLC-based skid for a single product line. Over five years, the plant expands to three production lines (1,200 I/O total) with batch recipes, regulatory control, and quality tracking.\n\n**Challenges encountered:** The PLC architecture required manual data logging via a SCADA database with limited historian capability. Recipe management relied on paper-based procedures. Expansion required adding a new PLC for each line with separate programming, leading to tag inconsistencies and increased maintenance overhead.\n\n**Solution:** The plant migrated to a Siemens PCS neo DCS. Existing PLC I/O was re-used via PROFINET gateways. Batch recipes were loaded into the DCS batch manager. The single engineering database eliminated tag duplication. Historian and reporting were integrated natively.\n\n**Results:** Engineering efficiency improved 35% (measured by time to implement new recipes). Historian data quality enabled OEE tracking for the first time. The five-year TCO was 12% lower than the equivalent PLC expansion scenario due to reduced engineering and maintenance overhead at the 1,200-I/O scale.\n\n> ASP OTOMASYON A.Ş. and its subsidiaries OPCTurkey and ASP Dijital provide end-to-end industrial engineering solutions for process automation, data operations and AI.\n\n---\n\n## References & Further Reading\n\n1. [ISA-95 / IEC 62264 — Enterprise-Control System Integration](https://www.isa.org/standards-and-publications/isa-standards/isa-95-standard) — International standard providing the functional hierarchy model that defines the roles of DCS and PLC/SCADA systems in manufacturing operations.\n2. [ABB Ability System 800xA — DCS Platform](https://new.abb.com/control-systems/system-800xa) — Official ABB documentation for their flagship distributed control system, including architecture, controller specifications, and redundancy features.\n3. [Siemens Process Automation — PCS 7 and PCS neo](https://www.siemens.com/global/en/products/automation/industry-software/process-automation.html) — Official Siemens documentation for DCS and process automation platforms, including migration guidance from legacy systems.\n4. [Rockwell Automation — PLC/SCADA Architecture Guide](https://www.rockwellautomation.com/en-us/products/software/factorytalk/designsuite/studio-5000.html) — Official Rockwell documentation on PLC-based control system design, scalability, and integration with plant-wide systems.\n5. [IEC 61131-3 — Programmable Controllers Programming Languages](https://www.iec.ch) — International standard covering the programming languages used in both PLC and DCS engineering environments for control logic development.\n\n## Use requirements, not fixed platform stereotypes\n\nModern DCS and PLC-based solutions overlap in execution capability, redundancy, and integration. Compare how each proposed system meets the actual process, operating, engineering, and maintenance requirements. Ask for a common scope including lifecycle support, licenses, alarm management, historian interfaces, source projects, and recovery. Generic I/O counts, scan ranges, or cost percentages are not procurement acceptance criteria.\n\nContinue with [the related practical guide](https://wiki.aspotomasyon.com/article/automation-rfq-scope-checklist).\n\n## Apply this to your project\n\n- Define the process states, timing requirements, and permitted behavior after a controller or communication failure.\n- List controller, I/O, network, software, and license dependencies before choosing an architecture.\n- Record acceptance results and prove that the delivered configuration can be restored from the handover package.\n\n[Follow an ASP project guide](https://wiki.aspotomasyon.com/guides) to connect the fundamentals with implementation and acceptance.\n\n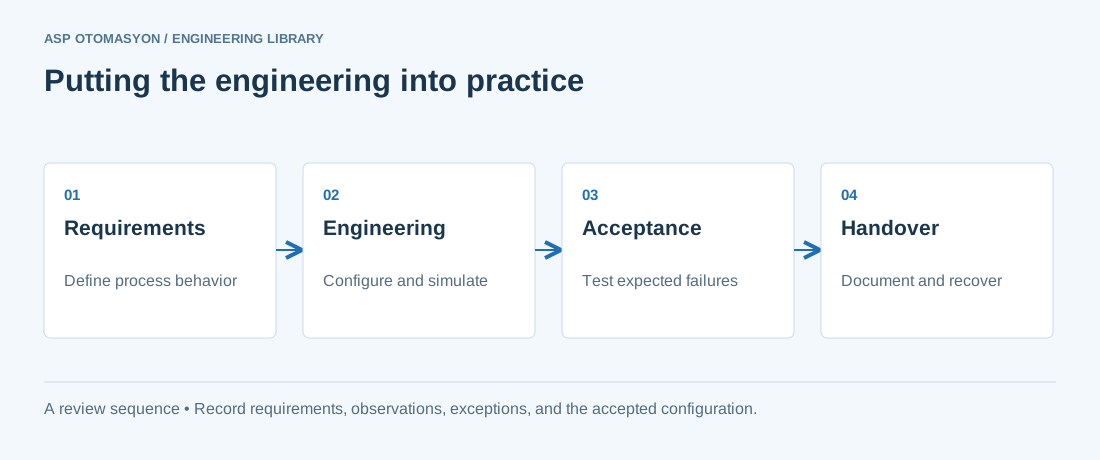\n\n*Engineering review sequence: Requirements → Engineering → Acceptance → Handover. Keep the recorded evidence with the accepted configuration.*\n\n## Primary references and further reading\n\nUse the original specifications and product documentation for implementation details. The examples in this guide are illustrative engineering scenarios, not published project results.\n\n- [NIST SP 800-82 Rev. 3 — OT architecture and security guidance](https://csrc.nist.gov/pubs/sp/800/82/r3/final)\n\n---\n\nCite the canonical article: https://wiki.aspotomasyon.com/article/dcs-vs-plc-selection-guide (DCS vs. PLC — A Comprehensive Selection Guide for Process Applications, ASP OTOMASYON, updated 2026-09-13).\n","headings":[{"id":"extended-decision-matrix-criterion-by-criterion-analysis","title":"Extended Decision Matrix — Criterion-by-Criterion Analysis"},{"id":"total-cost-of-ownership-by-project-size","title":"Total Cost of Ownership by Project Size"},{"id":"hybrid-dcsplc-architectures","title":"Hybrid DCS/PLC Architectures"},{"id":"vendor-comparison-when-each-platform-excels","title":"Vendor Comparison — When Each Platform Excels"},{"id":"migration-case-study-plc-to-dcs-as-a-plant-grows","title":"Migration Case Study — PLC to DCS as a Plant Grows"},{"id":"references-further-reading","title":"References & Further Reading"},{"id":"use-requirements-not-fixed-platform-stereotypes","title":"Use requirements, not fixed platform stereotypes"},{"id":"apply-this-to-your-project","title":"Apply this to your project"},{"id":"primary-references-and-further-reading","title":"Primary references and further reading"}],"faq":[],"references":[{"name":"ISA-95 / IEC 62264 — Enterprise-Control System Integration","url":"https://www.isa.org/standards-and-publications/isa-standards/isa-95-standard"},{"name":"ABB Ability System 800xA — DCS Platform","url":"https://new.abb.com/control-systems/system-800xa"},{"name":"Siemens Process Automation — PCS 7 and PCS neo","url":"https://www.siemens.com/global/en/products/automation/industry-software/process-automation.html"},{"name":"Rockwell Automation — PLC/SCADA Architecture Guide","url":"https://www.rockwellautomation.com/en-us/products/software/factorytalk/designsuite/studio-5000.html"},{"name":"IEC 61131-3 — Programmable Controllers Programming Languages","url":"https://www.iec.ch"},{"name":"NIST SP 800-82 Rev. 3 — OT architecture and security guidance","url":"https://csrc.nist.gov/pubs/sp/800/82/r3/final"}],"related":[{"slug":"industrial-energy-monitoring-systems","title":"Industrial Energy Monitoring Systems","summary":"Energy is one of the largest controllable costs in industrial manufacturing, typically representing 15–40% of total operational expenditure depending on the…","category":{"slug":"energy-management-systems","name":"Energy Management Systems"},"url":"https://wiki.aspotomasyon.com/article/industrial-energy-monitoring-systems","markdown_url":"https://wiki.aspotomasyon.com/article/industrial-energy-monitoring-systems.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/industrial-energy-monitoring-systems","published":"2026-05-13T11:58:29+00:00","modified":"2026-09-13T11:07:23+00:00","reading_minutes":9,"word_count":1808,"image":"https://wiki.aspotomasyon.com/assets/social/industrial-energy-monitoring-systems-8452ac92e5ef.png"},{"slug":"abb-800xa-dcs-architecture-configuration","title":"ABB 800xA DCS: Architecture and Configuration","summary":"The ABB Ability System 800xA is one of the most advanced Distributed Control Systems (DCS) available for process industries.","category":{"slug":"automation-systems","name":"Automation Systems"},"url":"https://wiki.aspotomasyon.com/article/abb-800xa-dcs-architecture-configuration","markdown_url":"https://wiki.aspotomasyon.com/article/abb-800xa-dcs-architecture-configuration.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/abb-800xa-dcs-architecture-configuration","published":"2026-05-13T12:07:53+00:00","modified":"2026-09-13T11:07:23+00:00","reading_minutes":9,"word_count":1882,"image":"https://wiki.aspotomasyon.com/assets/social/abb-800xa-dcs-architecture-configuration-6970a4d1cf7b.png"},{"slug":"smart-transmitter-configuration-calibration","title":"Smart Transmitter Configuration and Calibration","summary":"Smart transmitters represent the dominant technology in modern process instrumentation across oil and gas, chemical, pharmaceutical, power generation, and…","category":{"slug":"field-devices-instrumentation","name":"Field Devices & Instrumentation"},"url":"https://wiki.aspotomasyon.com/article/smart-transmitter-configuration-calibration","markdown_url":"https://wiki.aspotomasyon.com/article/smart-transmitter-configuration-calibration.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/smart-transmitter-configuration-calibration","published":"2026-05-13T12:07:56+00:00","modified":"2026-09-13T11:07:23+00:00","reading_minutes":8,"word_count":1735,"image":"https://wiki.aspotomasyon.com/assets/social/smart-transmitter-configuration-calibration-71c62d2b1655.png"},{"slug":"opc-ua-protocol-overview","title":"OPC UA Protocol Overview","summary":"OPC Unified Architecture (OPC UA) , defined by IEC 62541, is the platform-independent, service-oriented architecture for secure, reliable data exchange in…","category":{"slug":"opc-solutions","name":"OPC Solutions"},"url":"https://wiki.aspotomasyon.com/article/opc-ua-protocol-overview","markdown_url":"https://wiki.aspotomasyon.com/article/opc-ua-protocol-overview.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/opc-ua-protocol-overview","published":"2026-05-12T12:47:31+00:00","modified":"2026-09-13T11:07:23+00:00","reading_minutes":4,"word_count":873,"image":"https://wiki.aspotomasyon.com/assets/social/opc-ua-protocol-overview-eae98061a685.png"}],"citation":"ASP OTOMASYON. DCS vs. PLC — A Comprehensive Selection Guide for Process Applications. Updated 2026-09-13. https://wiki.aspotomasyon.com/article/dcs-vs-plc-selection-guide"}}