
Artificial intelligence in manufacturing has moved past the hype cycle into a pragmatic toolset: machine learning models that predict, classify, and optimize using the data plants already collect. The successful applications share a pattern — a narrow, well-defined problem, decent data history, and a clear decision the model informs. This article separates what works from what sells, and gives a framework for evaluating industrial ML projects.
Four application families dominate industrial ML deployments:
\n\n| Application | What the model does | Typical payoff |
|---|---|---|
| Predictive maintenance | Detects degradation patterns in vibration, temperature, current, and acoustic data; estimates remaining useful life. | Fewer unplanned stops, longer intervals between planned maintenance, fewer secondary failures. |
| Quality prediction and classification | Predicts defect likelihood from process parameters (temperature profiles, pressures, material lots) or classifies defects from vision data. | Earlier intervention, reduced scrap, fewer escapes. |
| Process optimization | Finds operating setpoints that minimize energy or maximize yield within constraints (soft-sensors, recommender models). | 1–5% efficiency gains in energy-intensive processes. |
| Anomaly detection | Learns normal behavior of machines or processes and flags deviations — the foundation of condition monitoring at scale. | Faster response to abnormal operation, fewer silent degradations. |
Energy forecasting, demand forecasting, and scheduling optimization round out the list; they share the same discipline.
\n\nBefore any model work, audit the data the project would use:
\n\nRule of thumb: if the plant cannot currently answer \"what happened to this asset in the last 6 months\" from its data, fix that before starting ML.
\n\nThe technology is rarely the bottleneck:
\n\nIndustrial ML works when it is narrow, data-backed, and decision-anchored: predictive maintenance, quality prediction, optimization, and anomaly detection — each built on audited data, a baseline, time-split validation, a shadow deployment, and an owned model lifecycle. The pattern repeats: data reality first, simple models first, trust before autonomy, and operations discipline from day one. That is how manufacturing turns analytics into results.
Follow an ASP project guide to connect the fundamentals with implementation and acceptance.

Use the original specifications and product documentation for implementation details. The examples in this guide are illustrative engineering scenarios, not published project results.
","markdown":"# AI and Machine Learning in Manufacturing: Practical Applications\n\n> Artificial intelligence in manufacturing has moved past the hype cycle into a pragmatic toolset: machine learning models that predict, classify, and optimize…\n\n- Canonical URL: https://wiki.aspotomasyon.com/article/ai-ml-industrial-applications\n- Publisher: ASP OTOMASYON A.Ş. (ASP OTOMASYON Wiki)\n- Category: Digital Transformation\n- Published: 2026-08-11 · Updated: 2026-09-13\n- Reading time: 4 min · Language: English\n\nArtificial intelligence in manufacturing has moved past the hype cycle into a pragmatic toolset: machine learning models that predict, classify, and optimize using the data plants already collect. The successful applications share a pattern — a narrow, well-defined problem, decent data history, and a clear decision the model informs. This article separates what works from what sells, and gives a framework for evaluating industrial ML projects.\n\n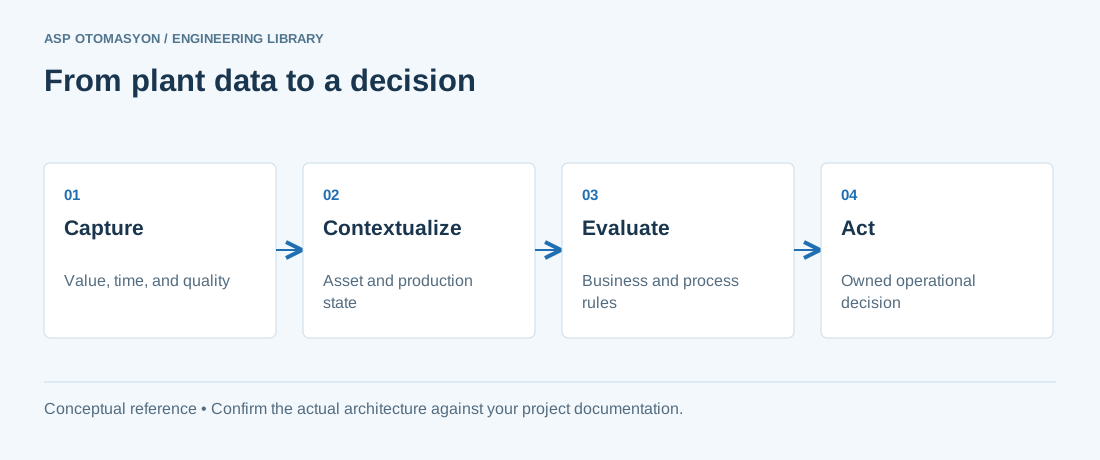\n\n*An industrial data workflow. Each handoff needs an owner and a documented data contract; collecting more signals alone does not establish business value.*\n\n## What Actually Works in Production\n\nFour application families dominate industrial ML deployments:\n\n| Application | What the model does | Typical payoff |\n| --- | --- | --- |\n| Predictive maintenance | Detects degradation patterns in vibration, temperature, current, and acoustic data; estimates remaining useful life. | Fewer unplanned stops, longer intervals between planned maintenance, fewer secondary failures. |\n| Quality prediction and classification | Predicts defect likelihood from process parameters (temperature profiles, pressures, material lots) or classifies defects from vision data. | Earlier intervention, reduced scrap, fewer escapes. |\n| Process optimization | Finds operating setpoints that minimize energy or maximize yield within constraints (soft-sensors, recommender models). | 1–5% efficiency gains in energy-intensive processes. |\n| Anomaly detection | Learns normal behavior of machines or processes and flags deviations — the foundation of condition monitoring at scale. | Faster response to abnormal operation, fewer silent degradations. |\n\nEnergy forecasting, demand forecasting, and scheduling optimization round out the list; they share the same discipline.\n\n## The Data Reality Check\n\nBefore any model work, audit the data the project would use:\n\n- **History depth** — models need data from *all* relevant states: healthy operation, degraded operation, and failures. If failures were rare and poorly recorded (most plants), the training set is missing its most important class — the standard cause of \"works in test, blind in production.\"\n- **Label quality** — the maintenance log, not the historian, provides the truth (\"bearing replaced 2024-03-12\"). Unstructured maintenance records must be cleaned and coded before they can label sensor data.\n- **Sampling alignment** — sensor data at 1 s, quality data per batch, maintenance events per incident: the model's feature table must align these on the asset and time axes — usually the largest engineering effort.\n- **Sensor health** — calibration drift, stale values, and missing telemetry corrupt features silently; feature engineering must include data-quality flags.\n\nRule of thumb: if the plant cannot currently answer \"what happened to this asset in the last 6 months\" from its data, fix that before starting ML.\n\n## Project Methodology\n\n1. **Define the decision** — what will change when the model works? (Maintenance triggered earlier; operator setpoint suggested; part re-inspected.) Projects without a defined decision do not ship.\n2. **Baseline first** — measure the current state: what does the existing threshold-based alarm or rule do? ML must beat it after accounting for deployment cost.\n3. **Start simple** — classical methods (regression, random forest, anomaly statistics) beat deep learning on most tabular plant data with far less infrastructure. Deep learning earns its place in vision and time-series at scale.\n4. **Validate on time** — split data by time (train on months 1–10, test on months 11–12), never randomly; industrial data is autocorrelated and random splits flatter results.\n5. **Deploy with a shadow phase** — run the model in parallel with existing logic, recording predictions without acting on them; this produces the evidence the operators need to trust it.\n6. **Operate the model** — models degrade (new product variants, changed processes); define monitoring (prediction drift, data drift), retraining triggers, and an owner. A model without an owner is a liability.\n\n## Organizational Realities\n\nThe technology is rarely the bottleneck:\n\n- **Trust** — operators will not act on a black-box recommendation that contradicts their experience. Provide explanations (feature contributions), pilot on low-risk assets, and let the shadow phase build the evidence.\n- **Skills** — the plant needs data engineering and model operation skills; a model built by consultants and forgotten fails. Build internal ownership from the first pilot.\n- **IT/OT collaboration** — model inputs come from OT historians and outputs go to maintenance and production systems; the governance (who owns the model, who owns the data) must be agreed before deployment, not after.\n- **Scope discipline** — one pilot, one metric, one decision. The plants with ten successful narrow models are the ones that eventually attempt the ambitious platform.\n\n## Summary\n\nIndustrial ML works when it is narrow, data-backed, and decision-anchored: predictive maintenance, quality prediction, optimization, and anomaly detection — each built on audited data, a baseline, time-split validation, a shadow deployment, and an owned model lifecycle. The pattern repeats: data reality first, simple models first, trust before autonomy, and operations discipline from day one. That is how manufacturing turns analytics into results.\n\n## Apply this to your project\n\n- Name the operational decision, its owner, and the evidence required to judge whether it improved.\n- Document asset identifiers, units, timestamps, quality rules, and definitions shared between OT and business applications.\n- Compare the pilot against a recorded baseline before extending it to other machines or sites.\n\n[Follow an ASP project guide](https://wiki.aspotomasyon.com/guides) to connect the fundamentals with implementation and acceptance.\n\n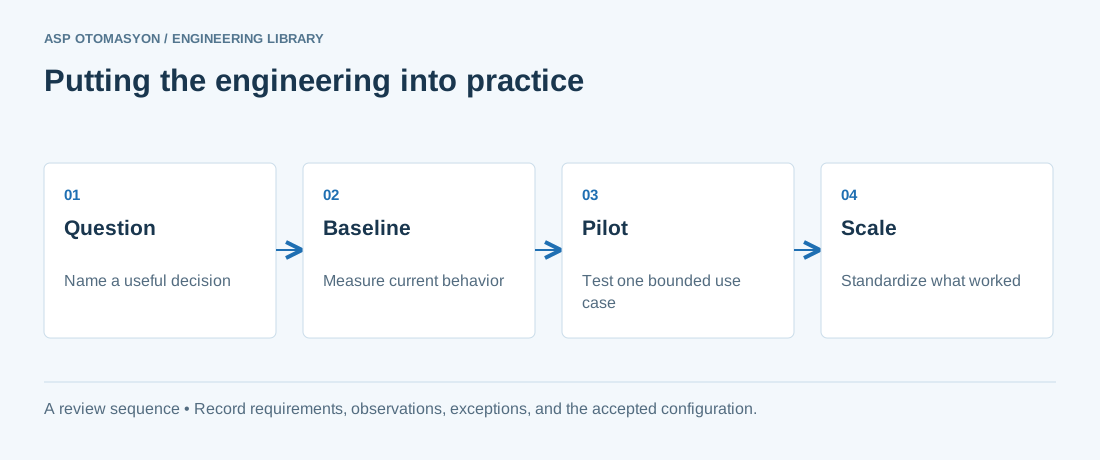\n\n*Engineering review sequence: Question → Baseline → Pilot → Scale. Keep the recorded evidence with the accepted configuration.*\n\n## Primary references and further reading\n\nUse the original specifications and product documentation for implementation details. The examples in this guide are illustrative engineering scenarios, not published project results.\n\n- [ISA — ISA-95 enterprise/control system integration](https://www.isa.org/standards-and-publications/isa-standards/isa-95-standard)\n- [OPC Foundation — Information modelling](https://opcfoundation.org/about/opc-technologies/opc-ua/)\n\n---\n\nCite the canonical article: https://wiki.aspotomasyon.com/article/ai-ml-industrial-applications (AI and Machine Learning in Manufacturing: Practical Applications, ASP OTOMASYON, updated 2026-09-13).\n","headings":[{"id":"what-actually-works-in-production","title":"What Actually Works in Production"},{"id":"the-data-reality-check","title":"The Data Reality Check"},{"id":"project-methodology","title":"Project Methodology"},{"id":"organizational-realities","title":"Organizational Realities"},{"id":"summary","title":"Summary"},{"id":"apply-this-to-your-project","title":"Apply this to your project"},{"id":"primary-references-and-further-reading","title":"Primary references and further reading"}],"faq":[],"references":[{"name":"ISA — ISA-95 enterprise/control system integration","url":"https://www.isa.org/standards-and-publications/isa-standards/isa-95-standard"},{"name":"OPC Foundation — Information modelling","url":"https://opcfoundation.org/about/opc-technologies/opc-ua/"}],"related":[{"slug":"llm-rag-industrial-documentation-safe-deployment","title":"LLM Assistants for Plant Documentation: Safe RAG Deployment","summary":"A plant documentation assistant is safe only when it cites controlled revisions, respects source permissions, and stays read-only and advisory, which a fixed…","category":{"slug":"digital-transformation","name":"Digital Transformation"},"url":"https://wiki.aspotomasyon.com/article/llm-rag-industrial-documentation-safe-deployment","markdown_url":"https://wiki.aspotomasyon.com/article/llm-rag-industrial-documentation-safe-deployment.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/llm-rag-industrial-documentation-safe-deployment","published":"2026-10-11T11:46:21+00:00","modified":"2026-10-11T11:46:21+00:00","reading_minutes":9,"word_count":1927,"image":"https://wiki.aspotomasyon.com/assets/social/llm-rag-industrial-documentation-safe-deployment-40155621b146.png"},{"slug":"manufacturing-data-governance","title":"Manufacturing Data Governance: Ownership, Quality and Lineage","summary":"Industrial digitalization projects collect more data every year — historians, MES, quality systems, energy meters, edge devices — and then struggle with the…","category":{"slug":"digital-transformation","name":"Digital Transformation"},"url":"https://wiki.aspotomasyon.com/article/manufacturing-data-governance","markdown_url":"https://wiki.aspotomasyon.com/article/manufacturing-data-governance.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/manufacturing-data-governance","published":"2026-08-11T13:05:19+00:00","modified":"2026-09-13T11:07:23+00:00","reading_minutes":4,"word_count":866,"image":"https://wiki.aspotomasyon.com/assets/social/manufacturing-data-governance-a71162f39625.png"},{"slug":"machine-vision-integration","title":"Machine Vision System Integration for Industrial Inspection","summary":"Machine vision gives machines eyes: cameras and image-processing software that inspect, measure, locate, and identify parts at production speed.","category":{"slug":"automation-systems","name":"Automation Systems"},"url":"https://wiki.aspotomasyon.com/article/machine-vision-integration","markdown_url":"https://wiki.aspotomasyon.com/article/machine-vision-integration.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/machine-vision-integration","published":"2026-08-11T13:05:19+00:00","modified":"2026-09-13T11:07:23+00:00","reading_minutes":5,"word_count":884,"image":"https://wiki.aspotomasyon.com/assets/social/machine-vision-integration-0a455cbc5038.png"},{"slug":"iiot-sensor-integration-patterns","title":"IIoT Sensor Integration Patterns","summary":"Integrating industrial sensors into an Industrial Internet of Things (IIoT) architecture requires careful selection of sensor technologies, communication…","category":{"slug":"digital-transformation","name":"Digital Transformation"},"url":"https://wiki.aspotomasyon.com/article/iiot-sensor-integration-patterns","markdown_url":"https://wiki.aspotomasyon.com/article/iiot-sensor-integration-patterns.md","api_url":"https://wiki.aspotomasyon.com/api/v1/articles/iiot-sensor-integration-patterns","published":"2026-05-12T12:47:31+00:00","modified":"2026-09-13T11:07:23+00:00","reading_minutes":5,"word_count":965,"image":"https://wiki.aspotomasyon.com/assets/social/iiot-sensor-integration-patterns-083cebd7e251.png"}],"citation":"ASP OTOMASYON. AI and Machine Learning in Manufacturing: Practical Applications. Updated 2026-09-13. https://wiki.aspotomasyon.com/article/ai-ml-industrial-applications"}}